

In today's interconnected world, a product is only as strong as its weakest link. For textile brands and manufacturers, that link is often the global supply chain. Recent years have shown how quickly disruptions can occur, leading to costly delays and broken promises. That's why, beyond price and quality, supply chain stability has become the new cornerstone of a truly reliable partnership. This guide explains how to evaluate this critical factor and details how Taiyang Chemical builds resilience into every step of our process. When you partner with a reliable chemical supplier, you're not just buying chemicals; you're buying certainty. To mitigate your sourcing risk, start with a stable partner.
Why is supply chain stability so important? An unreliable supply of essential chemicals can have devastating consequences for your business.
A truly resilient global supply chain is not built by accident. It is the result of deliberate strategy and investment in four key pillars.
A supplier's own manufacturing capacity is the foundation. They must have the scale to meet your demands and, ideally, redundancy in their production capabilities to handle unexpected surges or maintenance.
Smart inventory management acts as a crucial buffer. This includes maintaining safety stocks of key raw materials and finished goods to insulate against short-term market fluctuations or shipping delays.
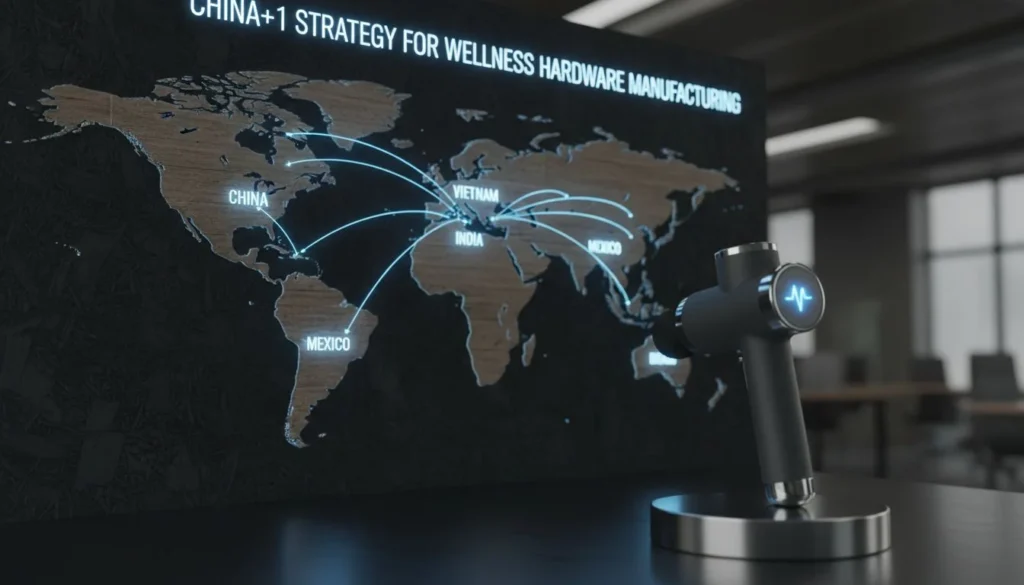
Relying on a single manufacturing location is a significant sourcing risk. A supplier with a diversified global footprint—multiple factories in different regions—can shift production if one location faces a disruption, ensuring continuity of supply.
Manufacturing the product is only half the journey. Strong, long-term relationships with reliable freight forwarders and logistics partnerships are essential for ensuring smooth and predictable on-time delivery.
At Taiyang Chemical, we have built our operations around these four pillars to be the reliable chemical supplier our global partners need.
We are a true chemical manufacturer with direct control over our production. Our strength lies in our diversified global footprint, with large-scale manufacturing facilities in two key locations: Dongguan, China, and Bình Dương, Vietnam. This dual-hub strategy provides a powerful layer of redundancy and flexibility.
Our inventory management is data-driven. We maintain strategic safety stocks of both raw materials and high-volume finished products. Our long-term relationships with raw material suppliers also help us mitigate the impact of price fluctuations and material shortages.
With over two decades of experience as a China textile chemical exporter, we have cultivated a network of trusted logistics partnerships. Our experienced export team manages the entire process, from documentation to final delivery, ensuring a smooth and transparent journey for your cargo.
When evaluating a new supplier, ask these critical questions:
A transparent and reliable chemical supplier should be able to answer these questions confidently.
In an unpredictable world, supply chain stability is the ultimate currency. It’s the assurance that your business can continue to operate, grow, and deliver on its promises. By choosing a partner like Taiyang Chemical, who has strategically invested in a resilient global supply chain, you are not just mitigating risk; you are building a foundation for a stronger, more successful future.
Secure your production against global uncertainties. Contact us to learn more about our resilient global supply chain and how we can support your business.
How do you manage raw material price fluctuations?
How do you manage raw material price fluctuations? While no one is immune to global market changes, our approach is twofold: first, our long-term relationships and bulk purchasing power with key raw material suppliers help us secure more stable pricing. Second, our strategic *inventory management allows us to buffer against sudden price spikes, providing our clients with greater predictability.
What is your contingency plan for a major disruption at one of your factory sites?
This is where our dual-factory strategy is key. Our contingency plan involves the ability to shift production of critical products between our facilities in China and Vietnam. This provides a level of redundancy that a single-location manufacturer cannot offer, ensuring continuity of supply during unforeseen events.
Can you support a Vendor-Managed Inventory (VMI) program for large-volume customers?
Yes. For our high-volume, long-term partners, we can develop Vendor-Managed Inventory (VMI) programs. This collaborative approach to inventory management helps to optimize stock levels, reduce carrying costs, and ensure a seamless supply of products.
How does your Vietnam factory contribute to your overall supply chain stability?
How does your Vietnam factory contribute to stability? Our Vietnam factory is a critical part of our supply chain stability strategy. It provides geographical diversification, mitigating risks associated with a single country. For our clients in Southeast Asia, it also offers a *local chemical supply chain, dramatically reducing lead times and transportation risks. To learn more, read our guide on our Vietnam operations.